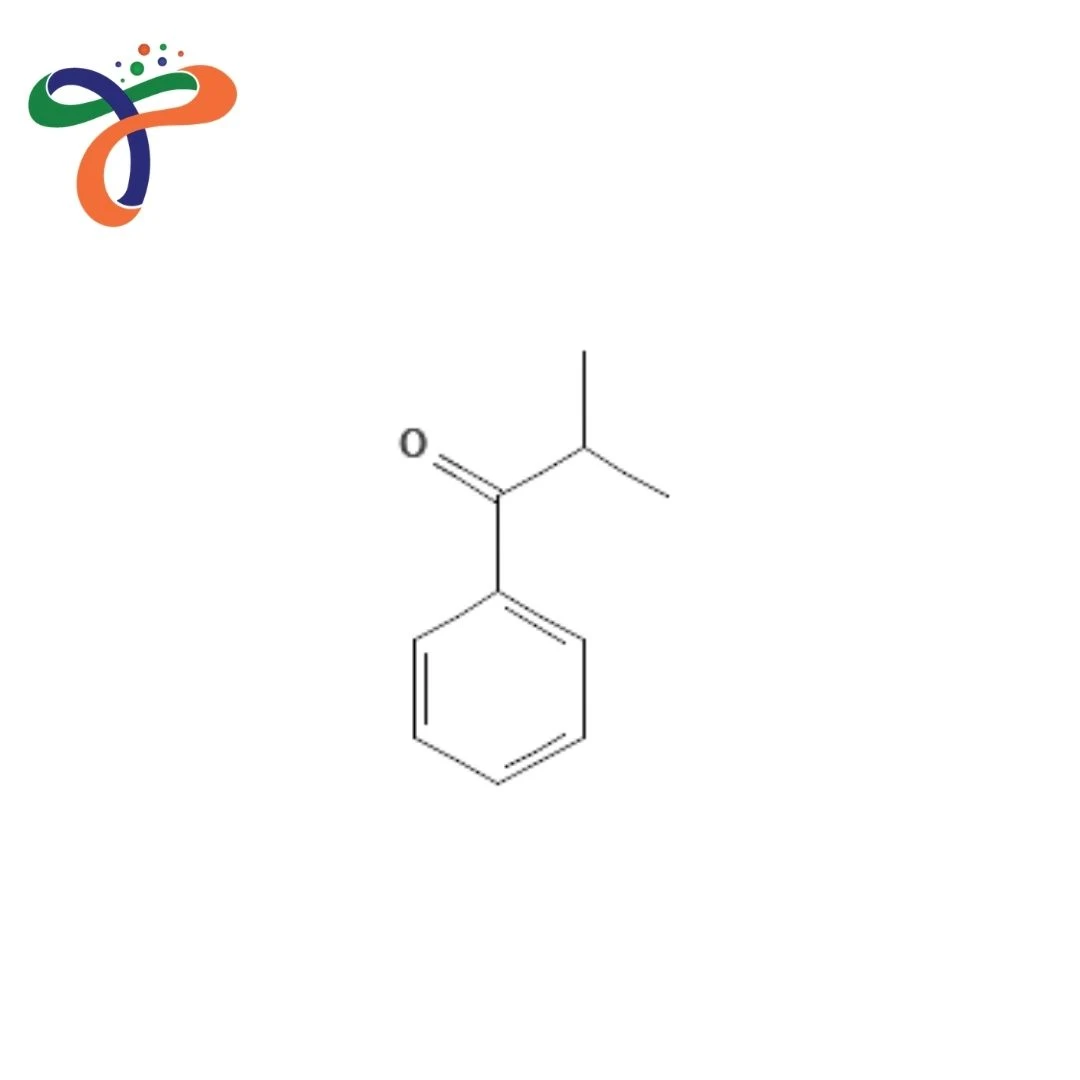
Isobutyrophenone | 611-70-1
Cas No :
611-70-1
Form :
Liquid
Molecular Weight :
148.20 g/mol
Molecular Formula :
C10H12O
Boiling Point :
236 °C
Melting Point :
-16 °C
Flash Point :
60 °C
Solubility :
Soluble in organic solvents, insoluble in water
Description :
Isobutyrophenone Manufacturer, Supplier, Distributor & Wholesaler | Chemical Bull
Overview
Chemical Bull is a trusted Isobutyrophenone manufacturer, supplier, distributor, and wholesaler in India. Produced under rigorous quality control standards and advanced organic synthesis protocols, our high-purity Isobutyrophenone, also known as 2-methyl-1-phenylpropan-1-one, is engineered to meet the exact assay limits, olfactory benchmarks, and purity standards required by global fragrance houses, flavor compounding units, and pharmaceutical synthesis laboratories.
As an indispensable aromatic ketone, Isobutyrophenone is widely valued for its characteristic sweet, floral, and fruity-balsamic odor profile, making it a crucial component in fine fragrances, cosmetic formulations, and specialty scent creations. Furthermore, it serves as a valuable intermediate in the synthesis of active pharmaceutical ingredients (APIs) and organic chemical building blocks. At Chemical Bull, our manufacturing and supply chain processes ensure batch-to-batch consistent olfactory purity, low trace impurity levels, and reliable bulk availability to support your commercial operations.
Why Choose Chemical Bull for Isobutyrophenone?
-
Verified Purity & Olfactory Consistency: Every batch of our isobutyrophenone undergoes advanced gas chromatography (GC) testing and sensory evaluation to ensure a minimum purity of 99% and a stable, clean odor profile free of heavy byproducts.
-
Direct Manufacturer Pricing: By eliminating intermediary channels, we provide highly competitive wholesale rates for bulk industrial consumers, fragrance houses, and chemical distributors, optimizing your raw material acquisition costs.
-
Robust Export Capabilities: As a leading participant in the global aroma and fine chemical market, we supply international standards-compliant shipments packaged in secure, inert containers.
-
Strict Quality Compliance: Every commercial order is dispatched with complete technical documentation, including verified Certificate of Analysis (CoA), Material Safety Data Sheet (MSDS), and Technical Data Sheet (TDS).
Rigorous Quality Control & Analytical Testing Protocols
To serve as your dependable aroma chemical partner, Chemical Bull implements a strict multi-tier quality assurance protocol. Every production batch undergoes comprehensive testing in our advanced testing laboratories:
-
Assay Verification: Tested via Gas Chromatography (GC) to ensure minimum 99.0% purity and eliminate off-notes.
-
Physical Property Screening: Precise refractive index and specific gravity checks at standard temperatures (20 C).
-
Traceability: Every consignment is dispatched with a batch-specific Certificate of Analysis (CoA) to guarantee complete transparency and regulatory compliance for your quality audits.
Key Applications Across Industries
-
Fragrance & Perfumery Formulation: Widely utilized in high-end fine fragrances, cosmetics, soaps, and household detergent scenting for its pleasant floral-balsamic nuance.
-
Flavor Compounding: Deployed in specialized food and beverage flavor compositions requiring subtle fruity and nutty aromatic notes.
-
Pharmaceutical & Organic Synthesis: Acts as a key reactive intermediate in synthesizing various organic compounds, specialized drugs, and fine chemical derivatives.
Industries We Serve
-
Global Fragrance Creation & Perfumery Compounding Houses
-
Cosmetics, Personal Care & Home Care Manufacturing Units
-
Active Pharmaceutical Ingredient (API) & Fine Chemical Synthesis Plants
-
Regulated Aroma Chemical Wholesale & Export Distributors
Frequently Asked Questions (FAQ)
-
Who are the leading Isobutyrophenone manufacturers and suppliers in India?
Chemical Bull is a trusted leading manufacturer, supplier, distributor, and wholesaler of high-purity Isobutyrophenone in India, serving global fragrance, flavor, and chemical industries with certified quality. -
What is the primary use of Isobutyrophenone?
It is primarily used as a high-grade aroma chemical for creating floral, fruity, and balsamic notes in perfumes and cosmetics, as well as an intermediate in organic synthesis. -
What purity assay does Chemical Bull guarantee for Isobutyrophenone?
We supply high-purity Isobutyrophenone with a certified GC assay of 9.0%, backed by batch-specific CoA documentation. -
How should Isobutyrophenone be stored to maintain its scent profile?
It should be stored in tightly sealed containers in a cool, dry, and well-ventilated warehouse away from direct sunlight, heat sources, and strong oxidizing agents. -
Do you support global export and technical documentation?
Yes, Chemical Bull supports international B2B buyers with secure export packaging and complete technical documentation, including MSDS, TDS, and Certificate of Analysis (CoA).
Isobutyrophenone MSDS
MSDS, TDS, and CoA documentation are readily available upon request to ensure safe handling, regulatory compliance, transport safety, and hazard communication for your plant operators.
Related Products Are
Secure Your Aroma Chemical Supply Chain with Chemical Bull Today
Partner with Chemical Bull for your continuous aroma chemical and fragrance ingredient sourcing requirements. Contact our expert team today to lock in competitive pricing, check real-time stock availability, or request a customized export quotation.
ChemicalBull supplies Isobutyrophenone across India, serving customers in Andhra Pradesh, Arunachal Pradesh, Assam, Bihar, Chhattisgarh, Goa, Gujarat, Haryana, Himachal Pradesh, Jharkhand, Karnataka, Kerala, Madhya Pradesh, Maharashtra, Manipur, Meghalaya, Mizoram, Nagaland, Odisha, Punjab, Rajasthan, Sikkim, Tamil Nadu, Telangana, Tripura, Uttar Pradesh, Uttarakhand, and West Bengal, as well as the Union Territories of Andaman & Nicobar Islands, Chandigarh, Dadra & Nagar Haveli and Daman & Diu, Delhi, Jammu & Kashmir, Ladakh, Lakshadweep, and Puducherry. We serve pharmaceutical, chemical, research, academic, laboratory, manufacturing, and industrial customers with reliable nationwide delivery.