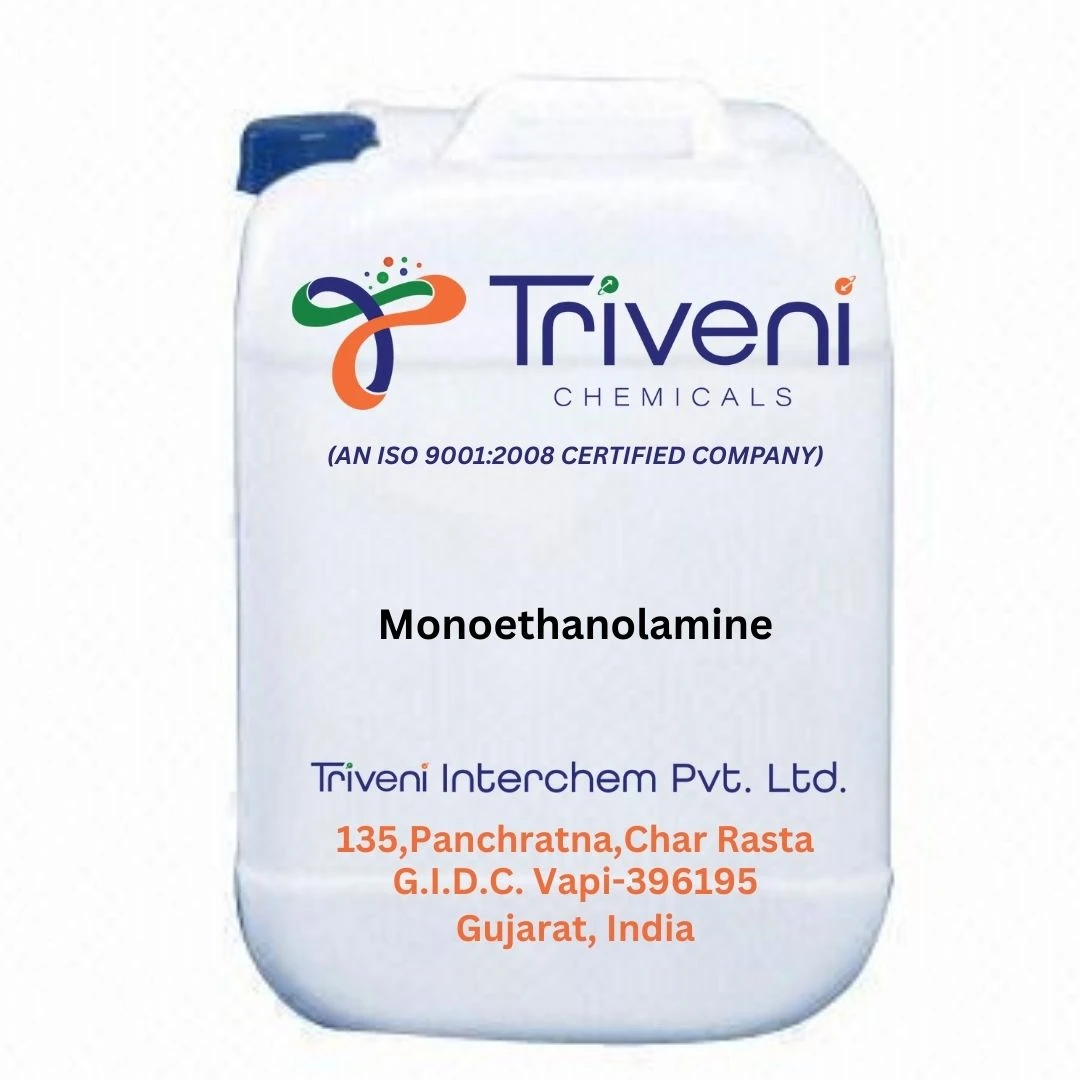
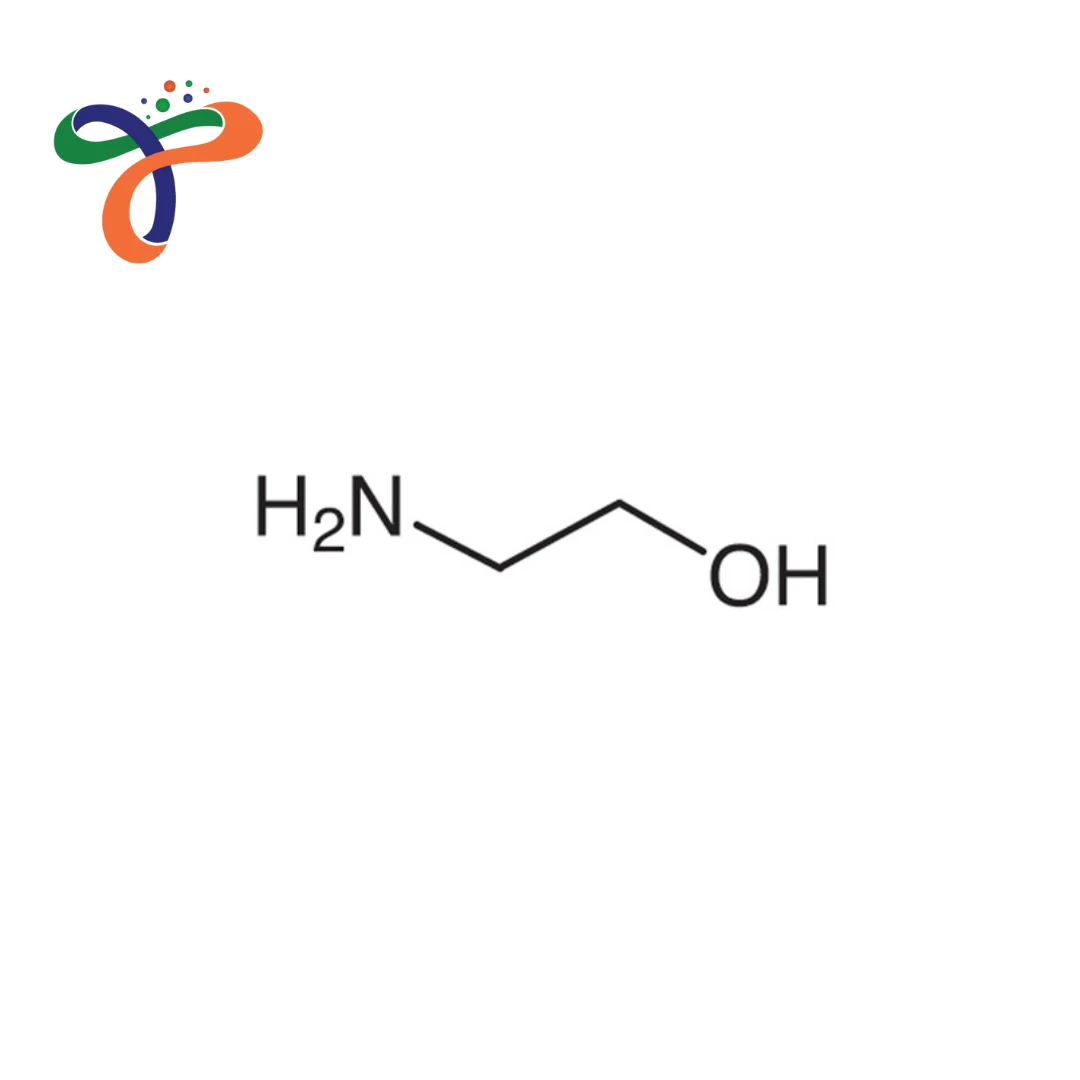
Monoethanolamine | 141-43-5
Cas No :
141-43-5
Form :
Liquid
Molecular Weight :
61.08 G/mol
Boiling Point :
170 °c
Melting Point :
-11 °c
Flash Point :
93 °c
Solubility :
Fully Miscible In Water
Description :
Monoethanolamine (MEA) Manufacturers, Suppliers, Distributors & Wholesaler | Chemical Bull
Overview
Chemical Bull is a trusted Monoethanolamine (MEA) manufacturer, supplier, distributor, and wholesaler in India. Produced under stringent quality control standards and advanced catalytic animation protocols, our high-purity Monoethanolamine (CAS Number: 141-43-5), also known as 2-aminoethanol or MEA, is engineered to meet the exact assay limits, color specifications, and high-performance standards required by global gas sweetening plants, detergent manufacturers, personal care formulators, textile auxiliary producers, and chemical synthesis units.
As a versatile organic compound containing both primary amine and primary alcohol functional groups, Monoethanolamine is globally renowned for its exceptional alkalinity, emulsifying power, and acid-gas absorption capabilities. It is widely utilized in natural gas and refinery units for removing carbon dioxide ($\text{CO}_2$) and hydrogen sulfide ($\text{H}_2\text{S}$) through gas sweetening processes. Furthermore, it serves as a crucial raw material in formulating heavy-duty liquid detergents, specialty surfactants, agricultural chemicals, and pharmaceutical intermediates. At Chemical Bull, our manufacturing and supply chain processes ensure batch-to-batch consistent active assay, ultra-low moisture retention, and reliable bulk availability to support your continuous commercial operations.
Why Choose Chemical Bull for Monoethanolamine?
-
Guaranteed High Assay & Low Moisture: Every batch of our Monoethanolamine undergoes rigorous acid-base titration and Karl Fischer testing to ensure a minimum purity of $99.0\%$ with strictly controlled water content, delivering optimal reaction and absorption efficiency.
-
Direct Manufacturer Pricing: By eliminating intermediary channels, we provide highly competitive wholesale rates for gas processing plants, detergent manufacturers, and chemical distributors, optimizing your bulk procurement costs.
-
Robust Export Capabilities: As a leading participant in the global industrial chemical market, we supply international standards-compliant shipments packaged in secure, corrosion-resistant containers.
-
Strict Quality Compliance: Every commercial order is dispatched with complete technical documentation, including verified Certificate of Analysis (CoA), Material Safety Data Sheet (MSDS), and Technical Data Sheet (TDS).
Rigorous Quality Control & Analytical Testing Protocols
To serve as your dependable chemical partner, Chemical Bull implements a strict multi-tier quality assurance protocol. Every production batch undergoes comprehensive testing in our advanced testing laboratories:
-
Assay Verification: Tested via standard hydrochloric acid titration to confirm exact active monoethanolamine percentage 99.0%.
-
Color & Moisture Screening: Precise APHA color scale checks and Karl Fischer moisture titration to ensure absolute clarity and prevent discoloration.
-
Traceability: Every consignment is dispatched with a batch-specific Certificate of Analysis (CoA) to guarantee complete transparency and regulatory compliance for your quality audits.
Safe Packaging & Global Export Logistics for Monoethanolamine
At Chemical Bull, we understand that maintaining chemical stability and protecting against atmospheric moisture and carbon dioxide absorption during transit is critical. We offer robust, export-compliant packaging solutions:
-
Packaging Options: Available in new, corrosion-resistant stainless steel drums, high-density polyethylene (HDPE) drums, intermediate bulk containers (IBC totes), and bulk tanker trucks.
-
Moisture & Carbon Dioxide Protection: Sealed hermetically under inert nitrogen blankets to prevent absorption of ambient moisture and $\text{CO}_2$ which can alter alkalinity.
-
Logistics & Compliance: Shipped in adherence to international transport safety regulations, ensuring safe delivery to your plant gates across India and global ports.
Key Applications Across Industries
-
Gas Sweetening & Refining: Widely utilized as an effective scrubbing solvent in amine gas treating units to remove acidic gases like H2S and CO2 from natural gas and refinery streams.
-
Detergents & Surfactants: Deployed as a neutralizing agent and building block in manufacturing liquid dishwashing soaps, laundry detergents, and industrial cleaners.
-
Personal Care & Cosmetics: Used as an emulsifier, surfactant, and pH adjuster in formulating shampoos, lotions, and cosmetic creams.
-
Textile Auxiliaries & Agrochemicals: Acts as a chemical intermediate in producing softening agents, dye levelers, and specialized agricultural herbicides.
Industries We Serve
-
Natural Gas Processing & Petroleum Refinery Plants
-
Industrial Detergent & Household Cleaner Manufacturing Units
-
Personal Care, Cosmetic & Emulsifier Formulation Enterprises
-
Textile Processing & Agrochemical Synthesis Plants
-
Global Industrial Chemical Wholesale & Export Distributors
Frequently Asked Questions (FAQ)
-
Who are the leading Monoethanolamine manufacturers and suppliers in India?
Chemical Bull is a trusted leading manufacturer, supplier, distributor, and wholesaler of high-purity Monoethanolamine in India, serving global gas processing, detergent, and chemical industries with certified quality. -
What is the primary industrial use of Monoethanolamine (MEA)?
It is primarily used in amine gas sweetening units to scrub acidic gases CO2 and H2S from natural gas and petroleum refinery streams, as well as an intermediate for detergents. -
What purity assay does Chemical Bull guarantee for Monoethanolamine?
We supply high-purity Monoethanolamine with a certified titration assay of 99.0%, backed by batch-specific CoA documentation. -
How should Monoethanolamine be stored to prevent degradation?
It should be stored in tightly sealed stainless steel or HDPE containers in a cool, dry, and well-ventilated warehouse away from strong acids, oxidizing agents, and direct exposure to air. -
Do you support global export and technical documentation?
Yes, Chemical Bull supports international B2B buyers with secure export packaging and complete technical documentation, including MSDS, TDS, and Certificate of Analysis (CoA).
Monoethanolamine MSDS
MSDS, TDS, and CoA documentation are readily available upon request to ensure safe handling, regulatory compliance, transport safety, and hazard communication for your plant operators.
Related Products:
Secure Your Industrial Chemical Supply with Chemical Bull Today
Partner with Chemical Bull for your continuous industrial chemical and solvent sourcing requirements. Contact our expert team today to lock in competitive pricing, check real-time stock availability, or request a customized export quotation.
ChemicalBull supplies Monoethanolamine across India, serving customers in Andhra Pradesh, Arunachal Pradesh, Assam, Bihar, Chhattisgarh, Goa, Gujarat, Haryana, Himachal Pradesh, Jharkhand, Karnataka, Kerala, Madhya Pradesh, Maharashtra, Manipur, Meghalaya, Mizoram, Nagaland, Odisha, Punjab, Rajasthan, Sikkim, Tamil Nadu, Telangana, Tripura, Uttar Pradesh, Uttarakhand, and West Bengal, as well as the Union Territories of Andaman & Nicobar Islands, Chandigarh, Dadra & Nagar Haveli and Daman & Diu, Delhi, Jammu & Kashmir, Ladakh, Lakshadweep, and Puducherry. We serve pharmaceutical, chemical, research, academic, laboratory, manufacturing, and industrial customers with reliable nationwide delivery.